Injection Moulding Machine for Wall Plugs and Rawl Plugs
Wall plugs are moulded on horizontal injection moulding machines in high-cavity moulds, usually from PA6 or PA66, with PE and PP for light-duty plugs. Cavity count sets the clamping force and shot weight more than plug size does. Dry the nylon properly, or the plug splits when the first screw goes in.
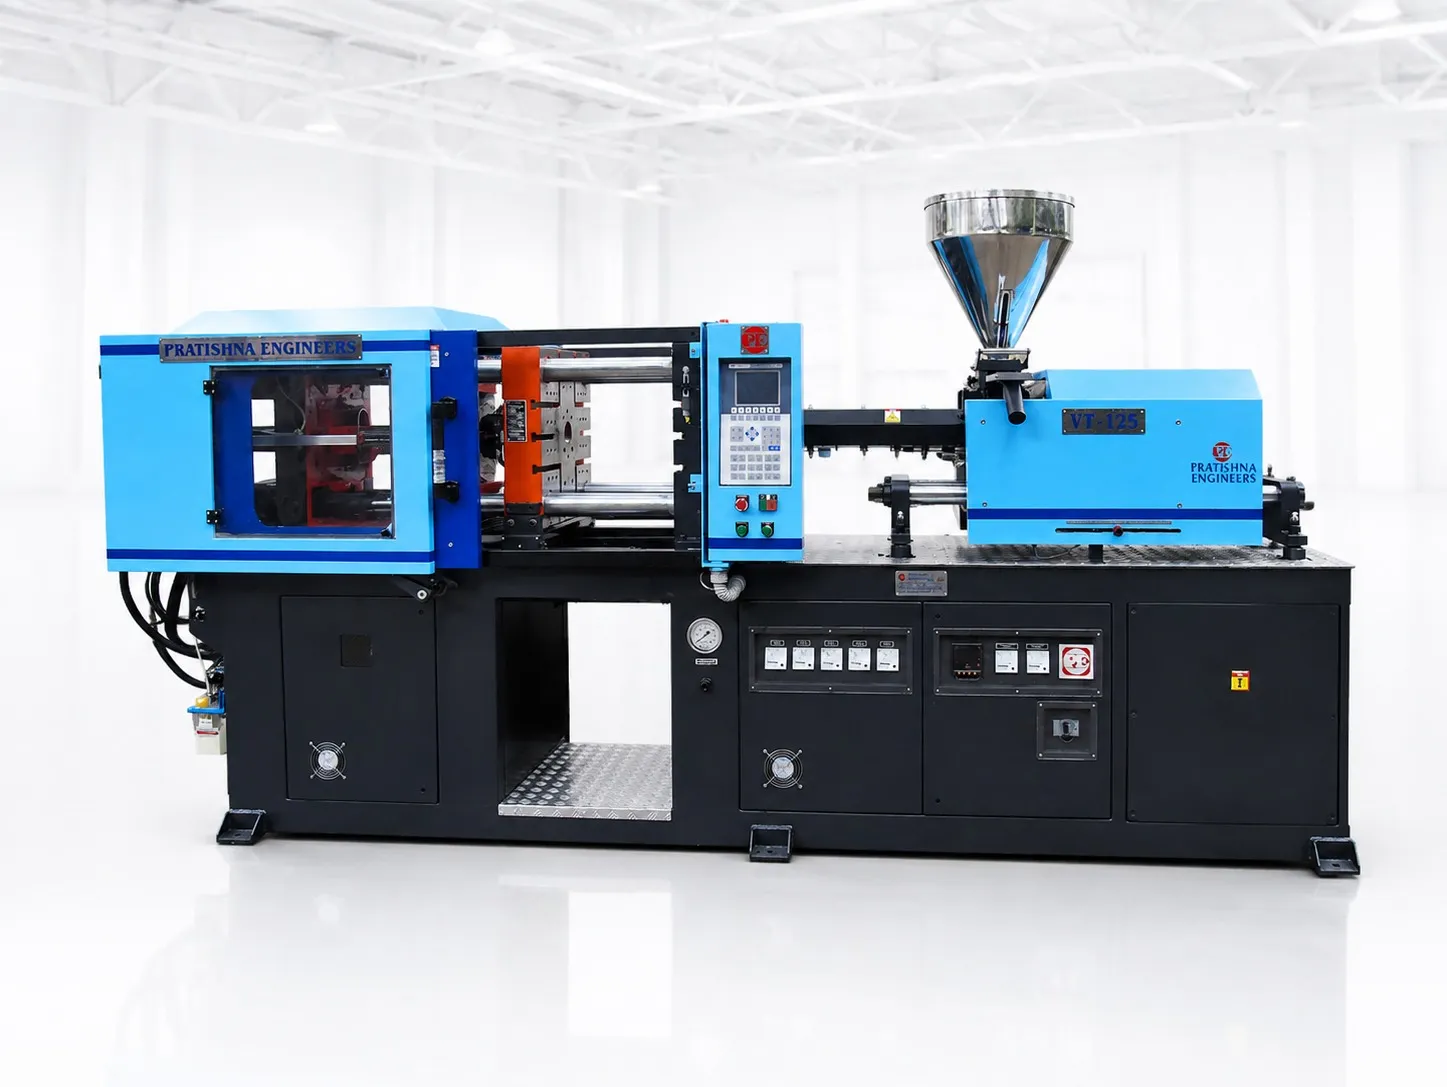
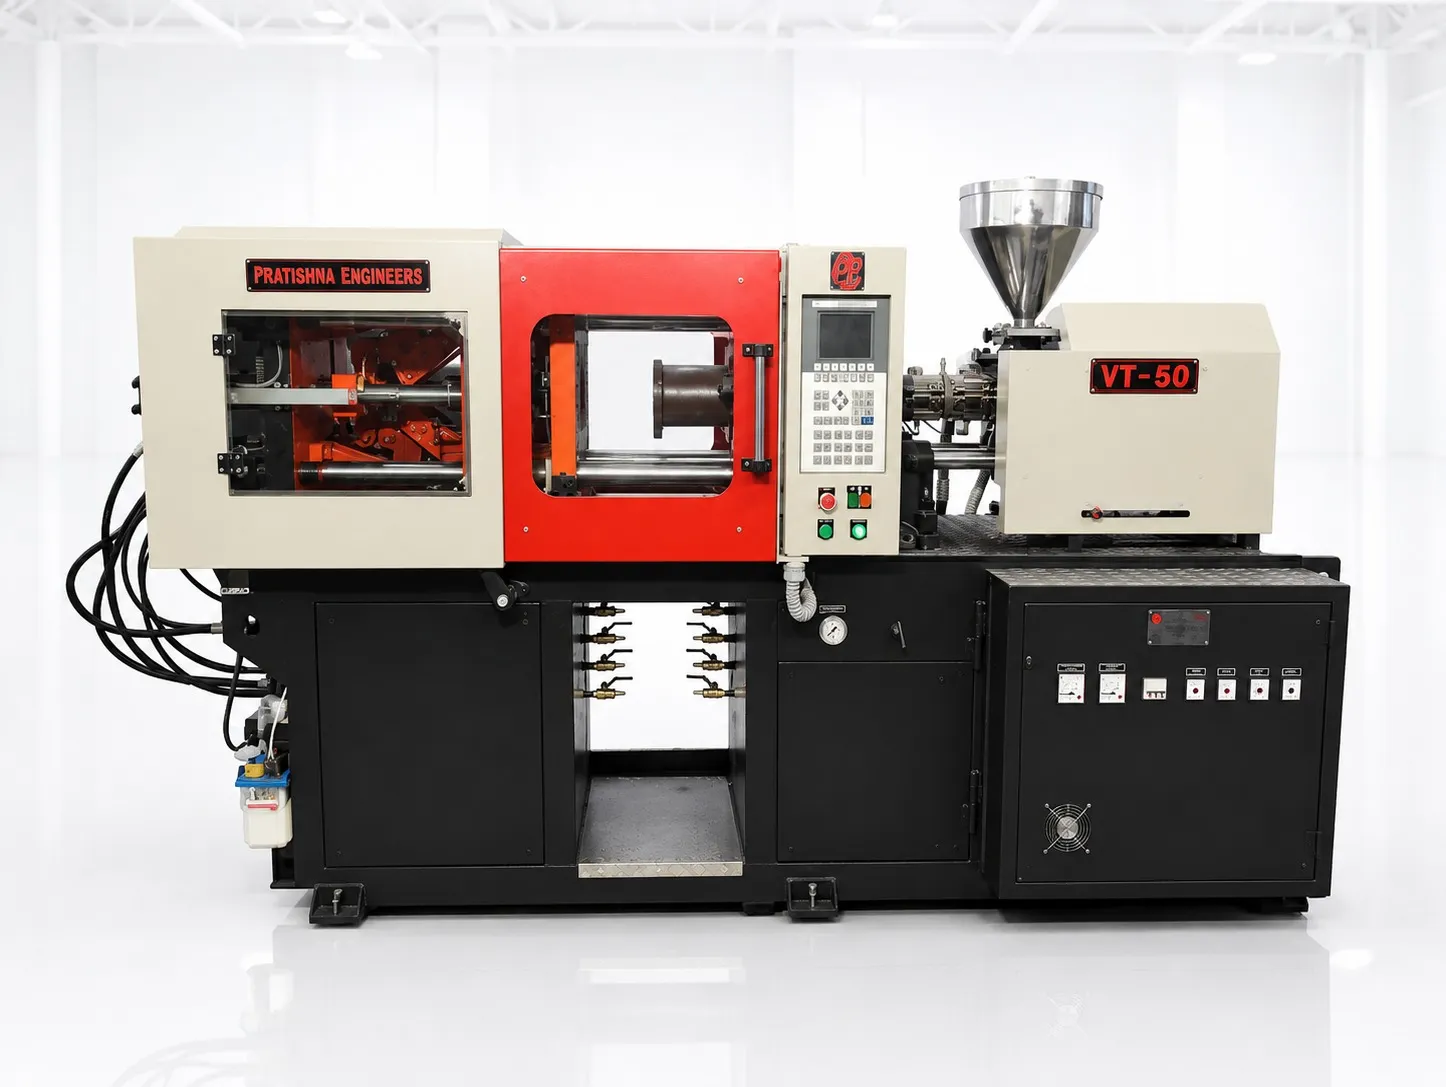
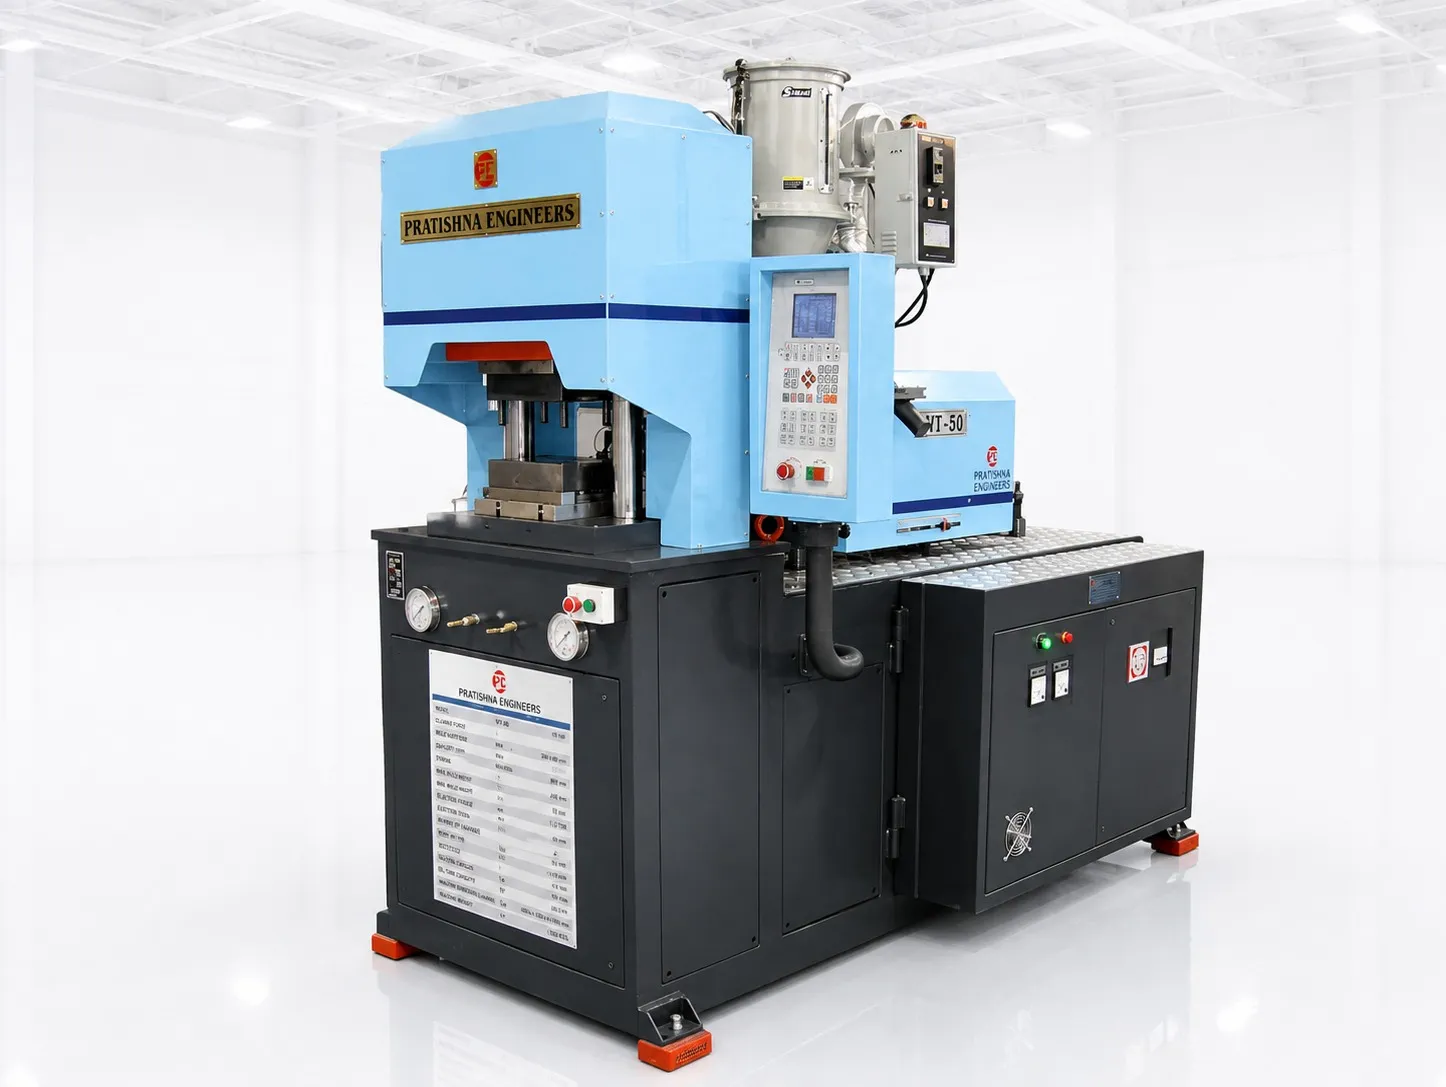
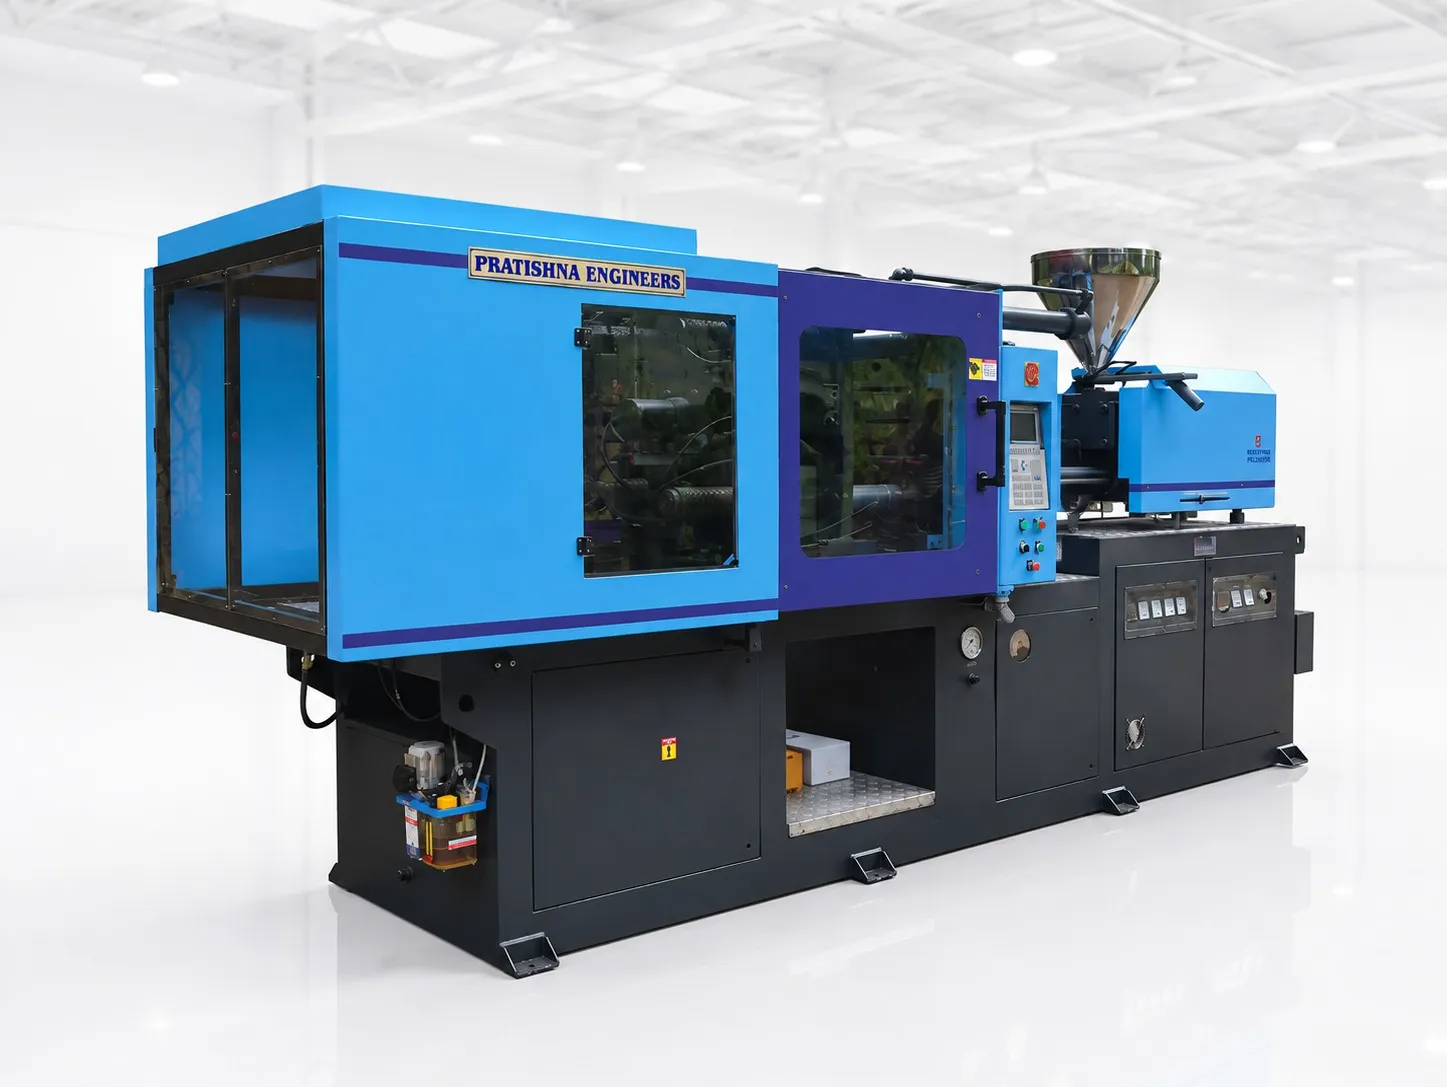
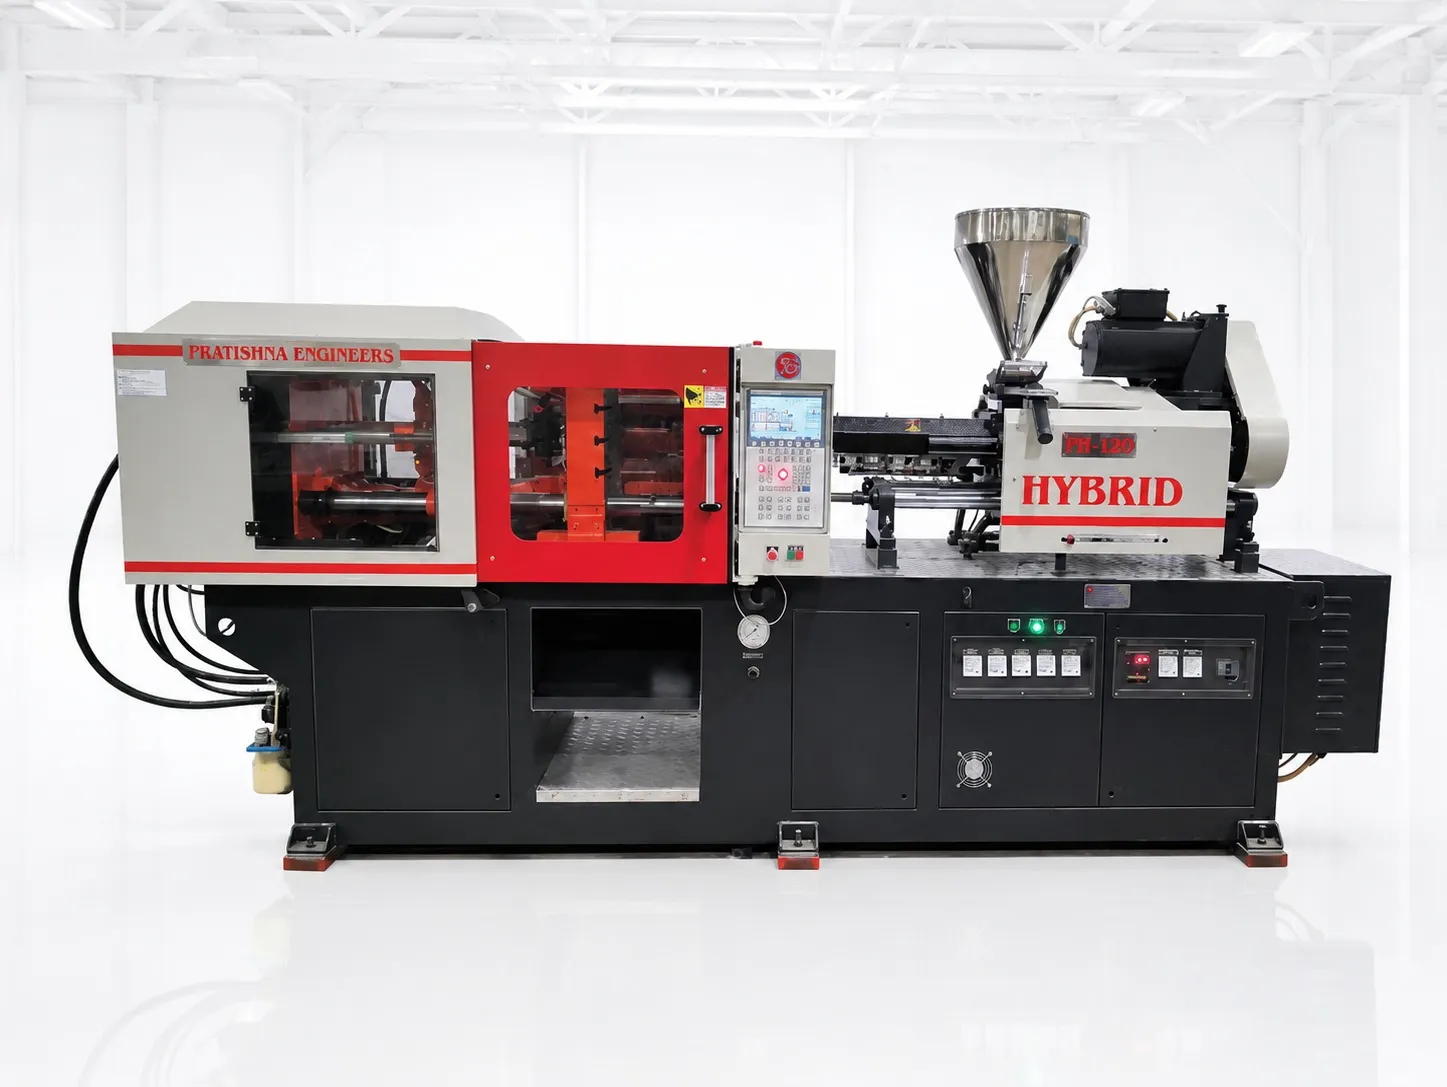
For plug tools, the press must carry many cavities with slides or collapsing cores and fill them evenly. Pratishna Engineers supplies horizontal injection moulding machines for wall plug production and can match a machine to the cavity count of your tool.
Manufacturing Wall Plugs?
Share the plug size range, material and cavity count, and Pratishna Engineers will recommend a machine for your tool.
Machine Requirements for Wall Plug Moulding
Plugs packed with furniture and wall-mount kits come from high-cavity tools with moving cores, so machine choice should cover:
- Clamping force and platen space for high-cavity tools
- Slides or collapsing cores for the split expansion zone
- Anti-rotation ribs filled fully in every cavity
- Nylon drying before moulding so plugs do not split
- Hardened hot runner parts or a cold runner layout
- Cavity balance so every plug expands the same
Recommended Machine for Wall Plugs
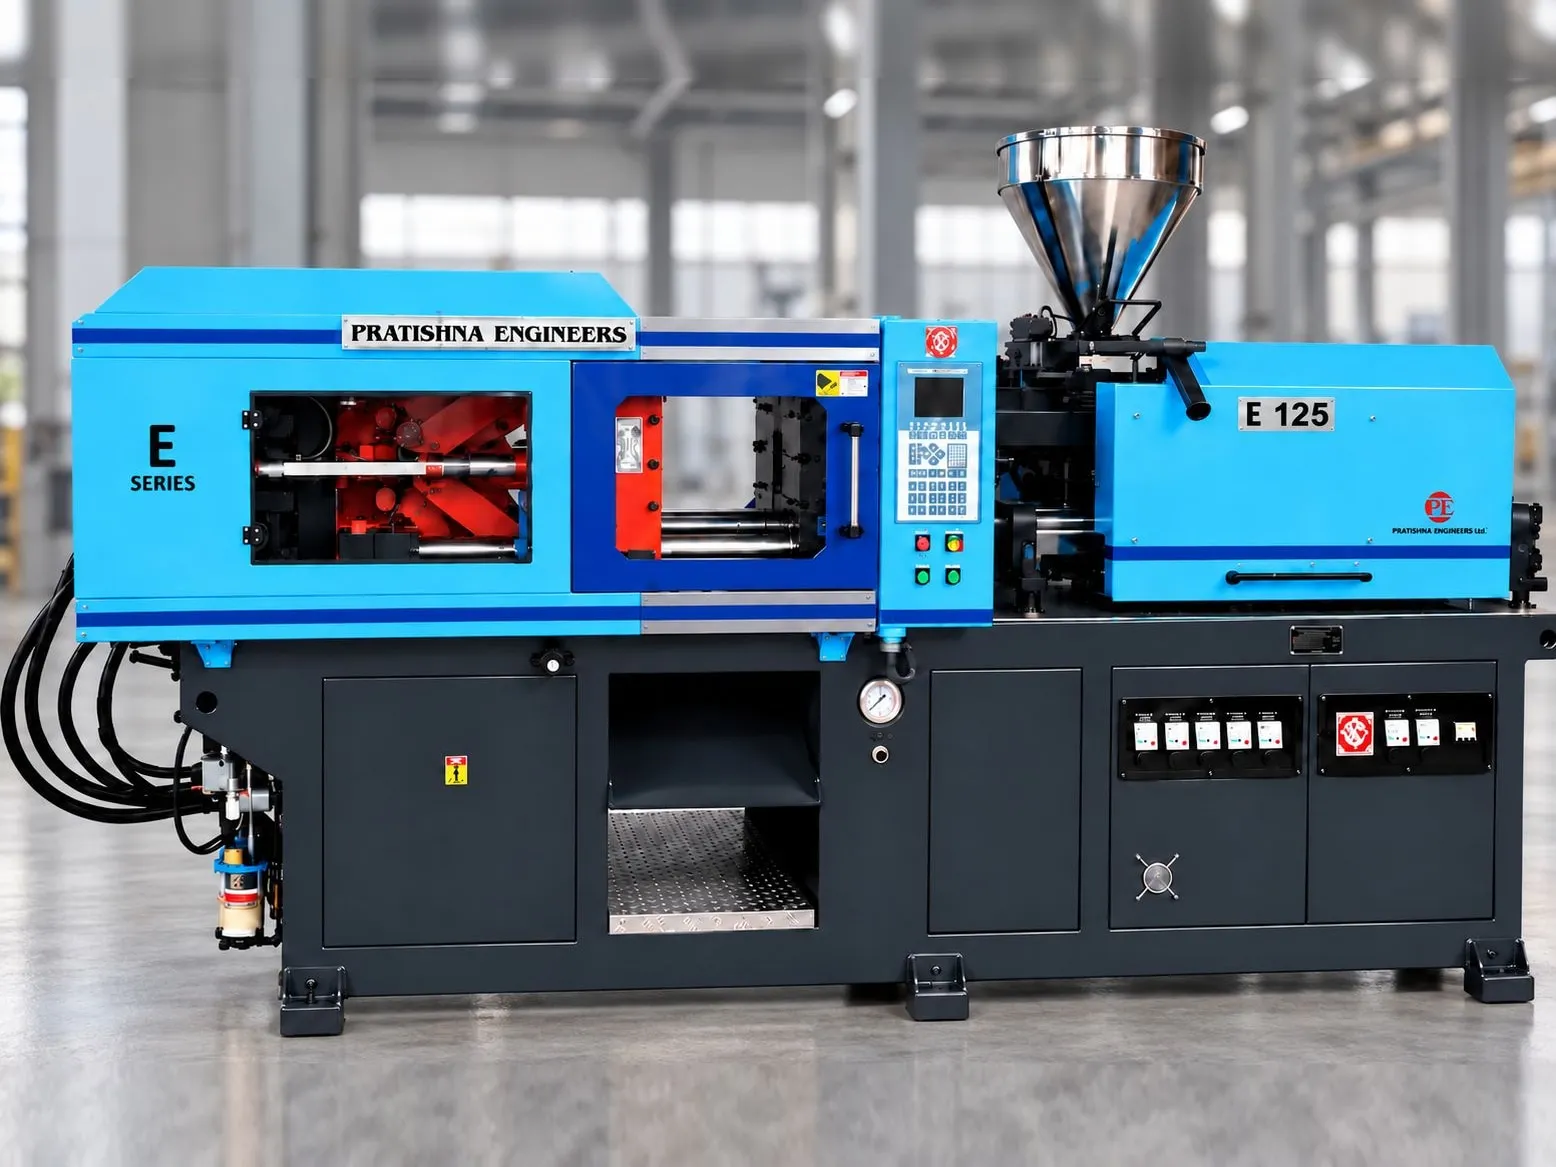
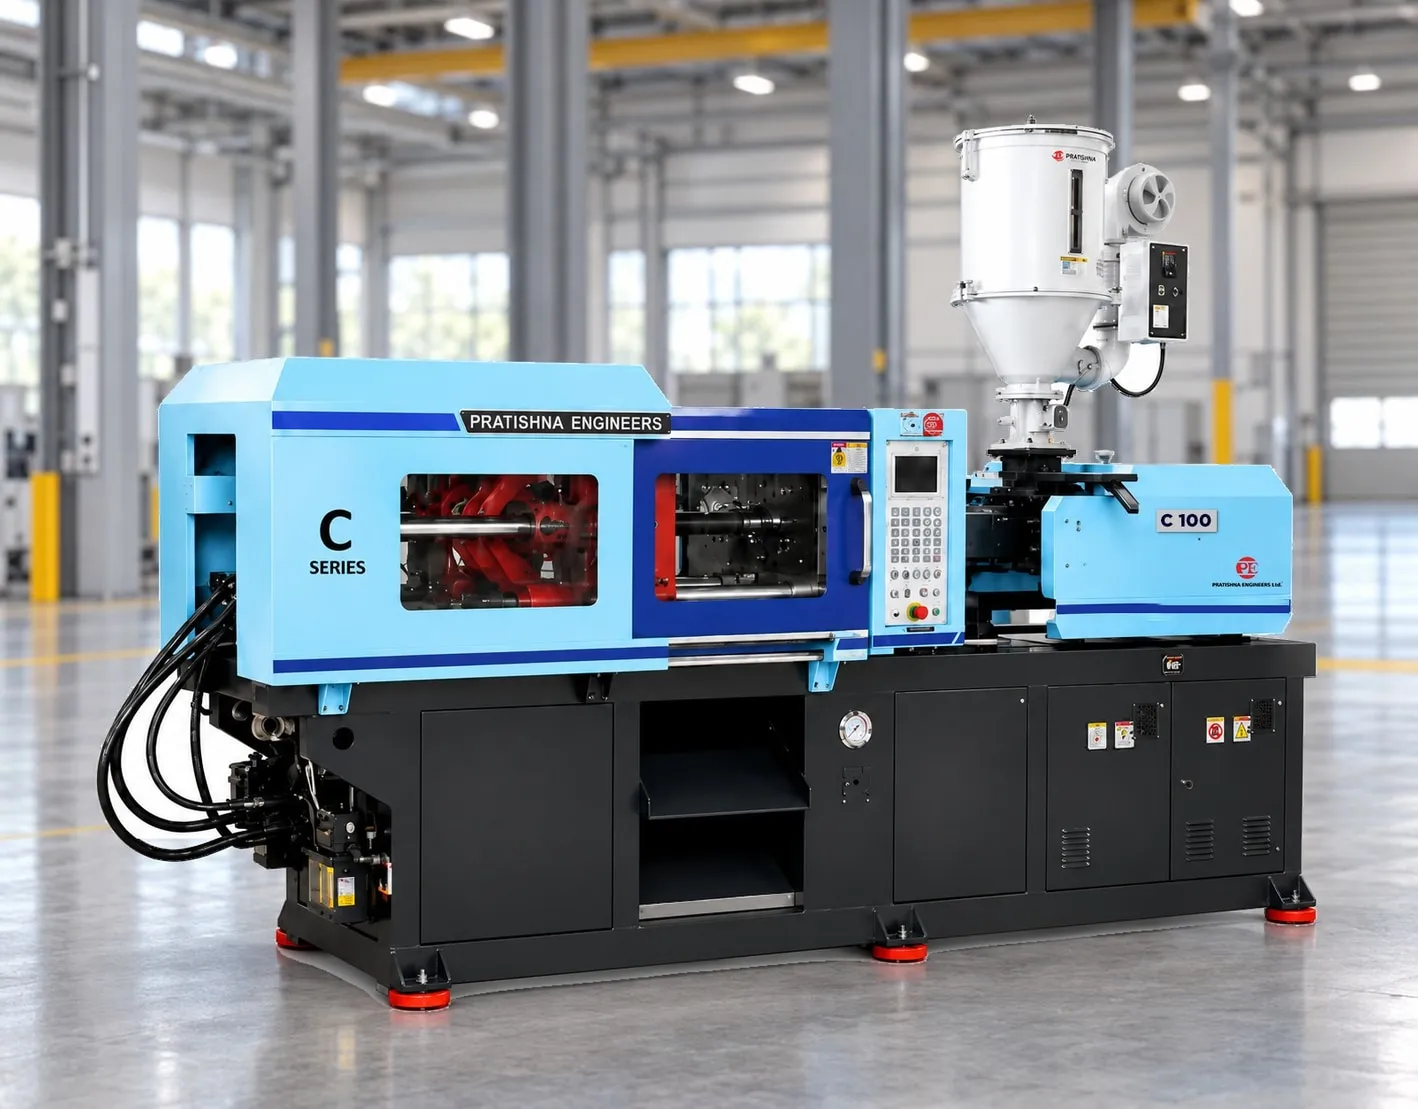
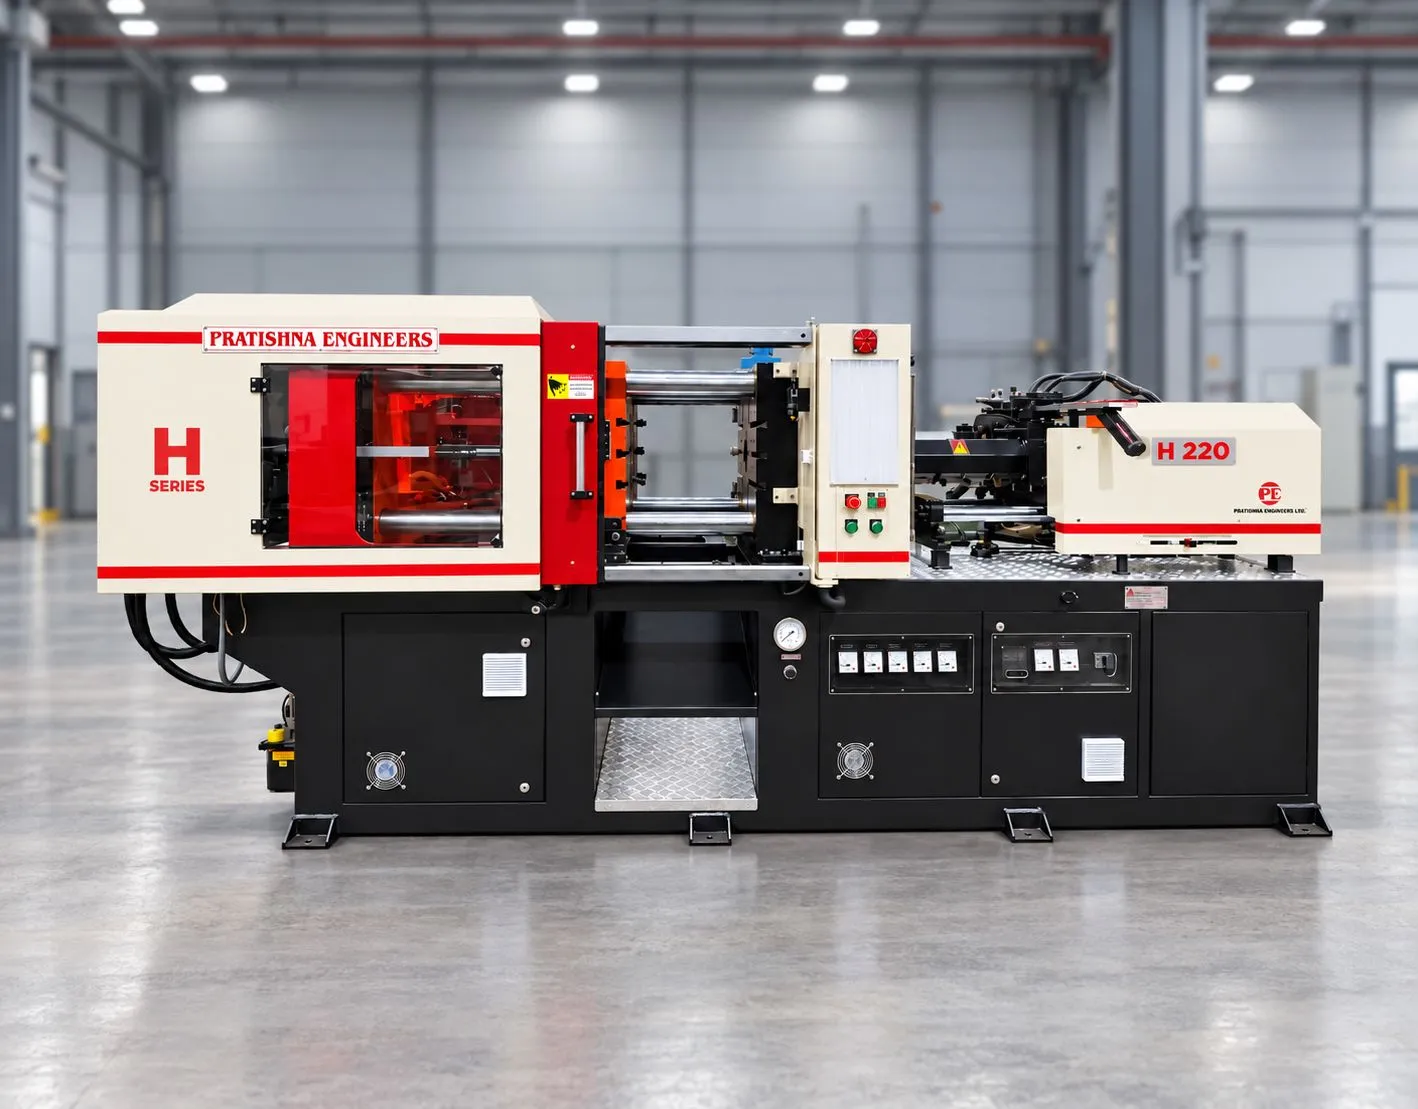
Small and mid-size plug tools suit the E Series (75-180 T). Higher-cavity moulds with slides move to the C Series (140-320 T), while the H Series (120-350 T) covers large multi-size tools and hot runner moulds. Tool makers often quote cavity count to suit the press, so plan the machine and the tool together.
Not Sure Which Machine You Need?
Share your plug range and target cavity count for a recommendation.
Why Choose Pratishna Engineers?
- Application-Based Machine Selection
- In-House Engineering & Manufacturing
- Multiple Machine Series
- Production-Focused Solutions
- End-to-End Technical Support
- Industry-Specific Solutions
- Machine Lifecycle Support
Injection Moulding Machine Buyer Resources
Download practical resources to help you select, size and specify the right machine.
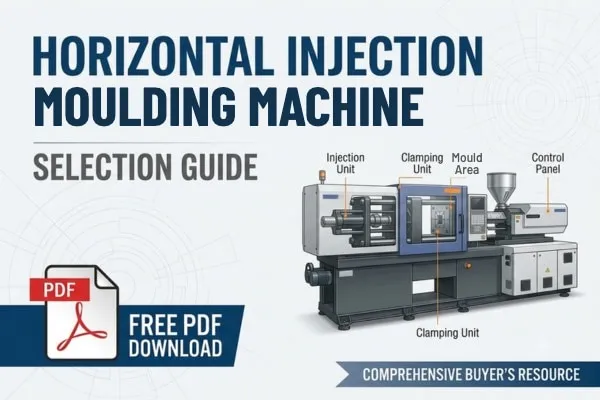
Horizontal Injection Moulding Machine Selection Guide
A step-by-step guide covering the key inputs needed to select the right machine: product weight, projected area, number of cavities, plastic material, required clamping force, shot / injection capacity, mould dimensions, production quantity, cycle time and automation requirement.
Download PDFPDF · 265 KB
How to Calculate Clamping Force for an Injection Moulding Machine
A clear methodology that explains how clamping force is calculated, covering projected area, injection pressure, safety factor, number of cavities and material considerations.
Download PDFPDF · 363 KBFurniture & Hardware Components & Machine Guide
A guide to Furniture & Hardware components, covering chairs, stools, tables, drawers, storage, hinges, drawer channels, knobs, castors and fittings. It explains large-part moulding, mould height, POM and nylon hardware, and how to match each part to a suitable machine.
Download PDFPDF · 203 KB
FAQs / Buyer Questions
Questions fixing and fastener makers ask about wall plug moulding.
Which Injection Moulding Machine Is Used to Make Wall Plugs?
The machine follows the tool. A modest-cavity plug mould fits the E Series, while higher-cavity or multi-size moulds need the C or H Series for platen area and shot capacity.Why Do Nylon Wall Plugs Split When a Screw Is Driven?
Undried nylon degrades in the barrel and moulds brittle. Freshly moulded plugs are also drier and more brittle than conditioned ones, so dry the resin to the supplier limit and test split resistance after conditioning too.Should a Wall Plug Mould Use a Hot or Cold Runner?
Cold runners are often the cheaper choice at this part size, with runners reground where the customer allows. Nylon hot runners need high-hardness components and close temperature control to avoid drooling and degradation.
How Are the Expansion Zone and Ribs Formed?
The split expansion zone and anti-rotation ribs are undercuts, so the tool uses slides or a collapsing core. These moving parts add mould height and need regular cleaning to avoid flash between cavities.Can Pratishna Recommend a Machine for My Wall Plug?
Yes. Share the plug sizes, drawings or samples, material, part weight, mould dimensions, cavity count and monthly volume, and Pratishna Engineers will recommend a suitable machine.Does the Machine Suit Other Fixing and Fastener Parts Too?
Yes. Similar machines mould anchor fasteners, fastener caps, push-fit and panel clips, and knock-down fittings such as dowels and shelf pins, subject to the mould.
Technical Disclaimer
Disclaimer: The information provided in this webpage is for general informational and educational purposes only. It is based on technical references and industry information available at the time of preparation and may be subject to change. It does not constitute engineering, technical, commercial or professional advice, nor does it constitute a quotation, specification, warranty or contractual commitment by Pratishna Engineers.
Actual injection moulding machine and process requirements vary according to the component design, material, mould, production volume, machine configuration and operating conditions. The information, examples, calculations and recommendations provided should be independently evaluated and verified for the specific application before making any equipment, process or production decision. Information obtained from third-party sources remains subject to the accuracy and limitations of those sources.
Limitation of Liability: Pratishna Engineers makes no representation or warranty, express or implied, regarding the completeness, accuracy or suitability of the information for any particular application. To the extent permitted by applicable law, Pratishna Engineers shall not be liable for any loss, damage, cost or consequence arising from reliance on or use of the information contained in this webpage. Final machine selection, configuration and application suitability should be confirmed with Pratishna Engineers based on complete and accurate project requirements.
Talk to Our Engineers
Planning a New Injection Moulding Project?
Share your component, material, mould and production target. Our engineering team will help you identify the right machine configuration.
- Machine Sales
- +91 99690 38542
- Service Support
- +91 97689 28259
- Sales Email
- [email protected]